Process Optimization
Nozzle Distance
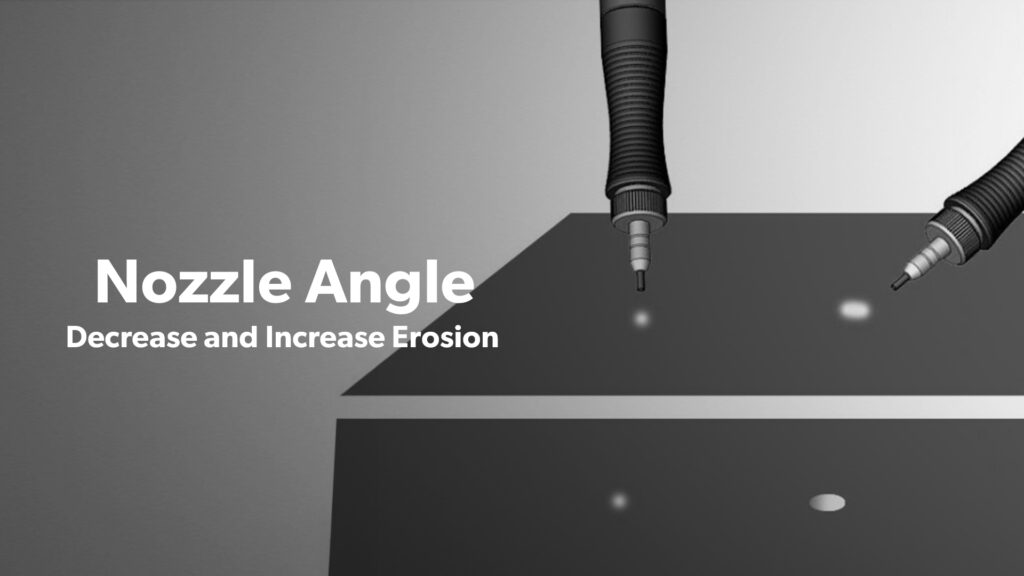

How far should you hold the nozzle from the part? There are a couple of factors which determine the ideal nozzle distance: abrasive velocity and the intent.
Abrasive velocity – as the abrasive exits the nozzle, it is accelerating. Therefore by holding the nozzle a bit further away you actually have a greater impact than holding the nozzle very close.
Intent – the purpose of blasting plays a role in finding the ideal distance from the part. Whether you’re trying to drill a hole for microfluidics, deburr an implant or texture a surface, there are different factors to consider when determining the ideal nozzle distance.
Let’s take a closer look at how intent sets the stage determining the ideal nozzle distance.
The long and short of Nozzle distance
Keep the Nozzle at a distance for Texturing applications
When held further away from the part, the nozzle gives a wide spray, providing good, even coverage for texturing applications.
The abrasive in the air stream will maintain velocity for several inches. By keeping the nozzle farther from the part, a more uniform finish is achieved. An added benefit is that a richer abrasive stream can be used becasue the particles are spread out over a greater spot size and will not interfere with each other.
Up Close and personal
When cutting or drilling through material with MicroBlasting, the nozzle should be held close to the part for a well defined cut. Cutting gorilla glass, etching precision channels for microfluidics or engraving lenses are just a few of applications which benefit from the nozzle held closer to the part.
Applications Landing in the Middle:
For deburring and coating removal applications, the ideal distance is somewhere between 0.25″ and 1″. This balances a focused abrasive stream with the benefits of a wider spray pattern.
Removing Coatings
Holding the nozzle at an angle effectively peels away coatings.
Deburring
Abrasive strikes the brittle root and chips off the rollover burr quickly without damage to the base material. Sweeping over the part keeping the nozzle in constant motion also help attack the burr from different directions, maximizing the impact without focusing too much in one spot which could potentially affect the surrounding surface.
Applications Lab
Let our experts help find the right solution for your part. We know no two applications are the same. Our Technical Specialists manage sample-part testing and processing from start-to-finish. They actively collaborate with our Sales and Engineering Teams while remaining completely accessible to you throughout the process.


Questions about MicroBlasting?
If you have questions about nozzle distance or how to refine the process specific to your application, contact me: